Case / 01Brownfield
BrownfieldF&B
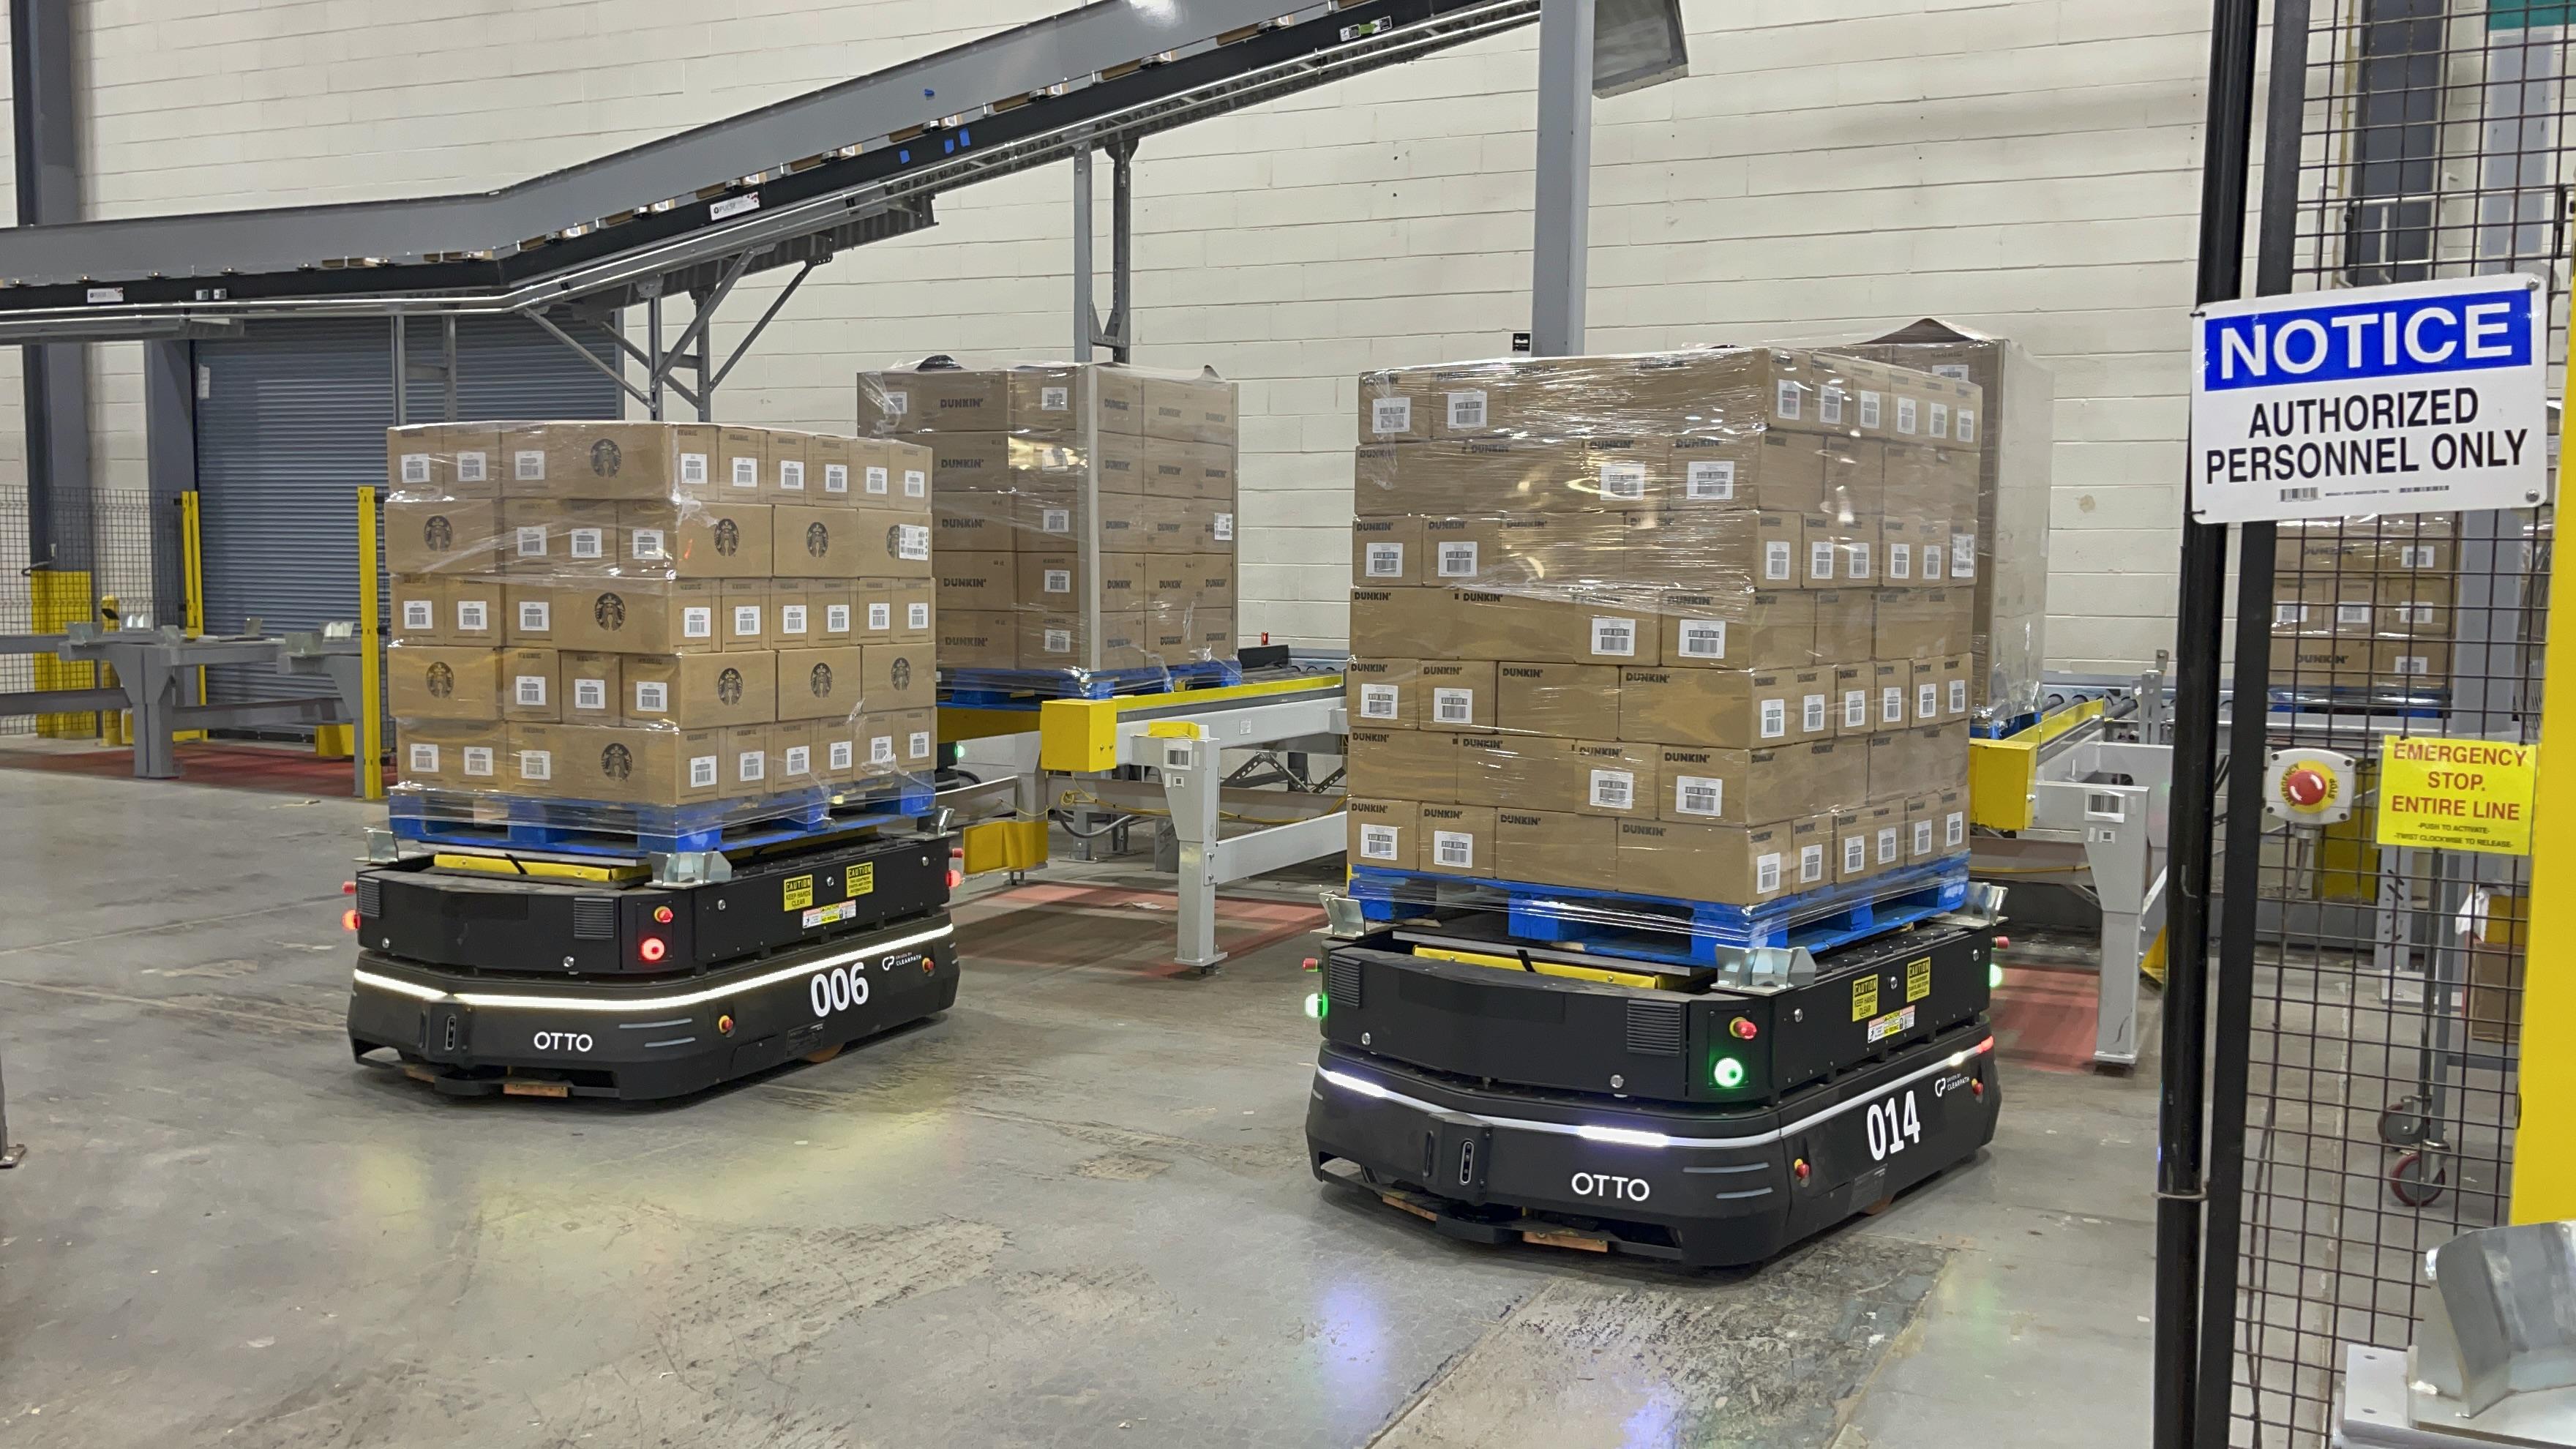
Brownfield Retrofit Across 30+ Packaging Lines
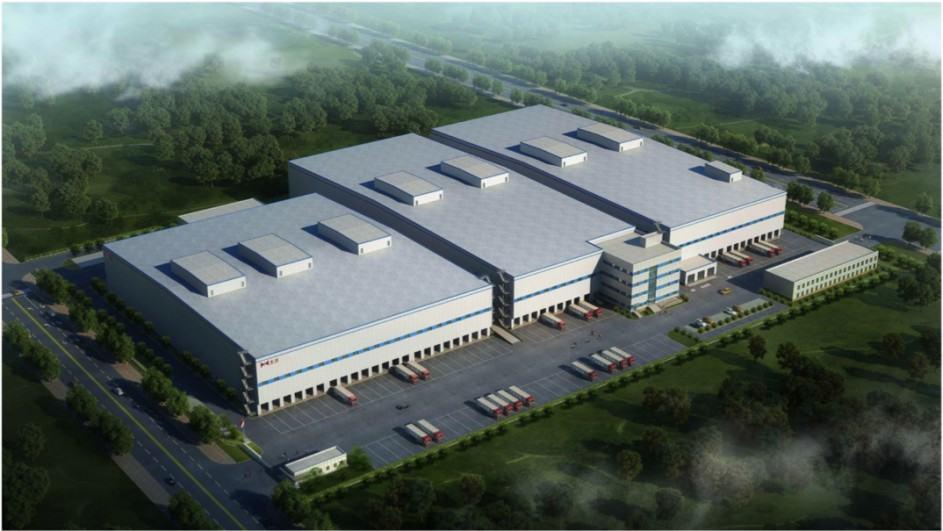
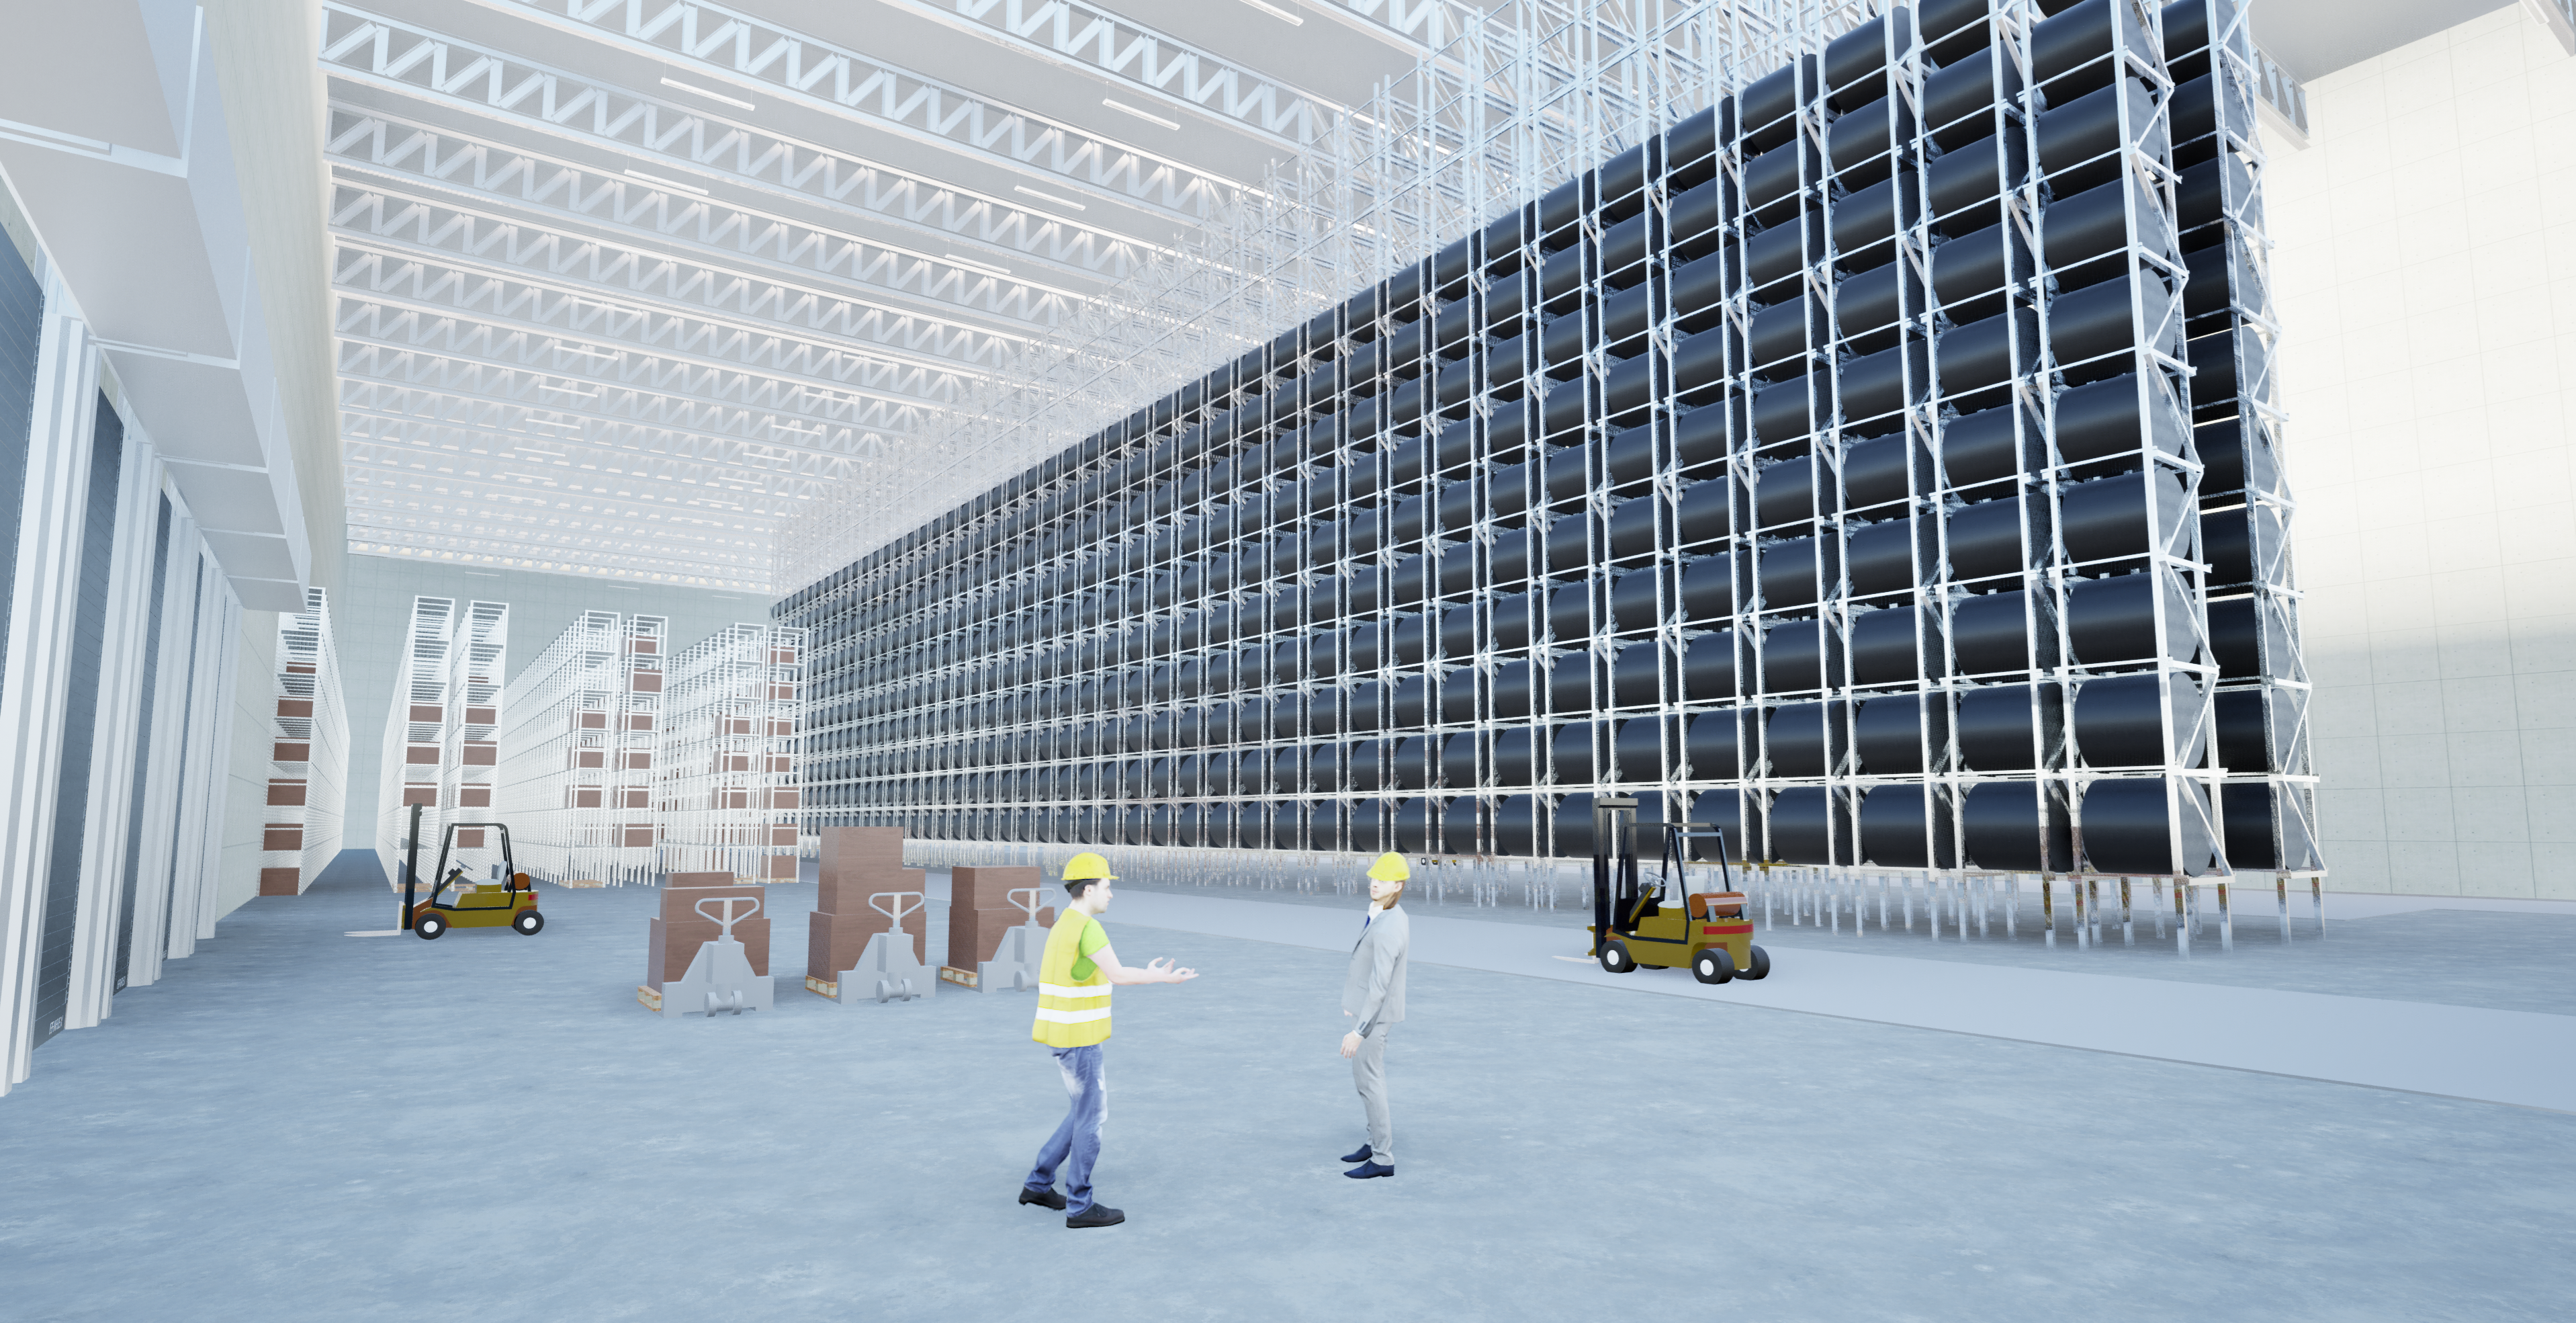
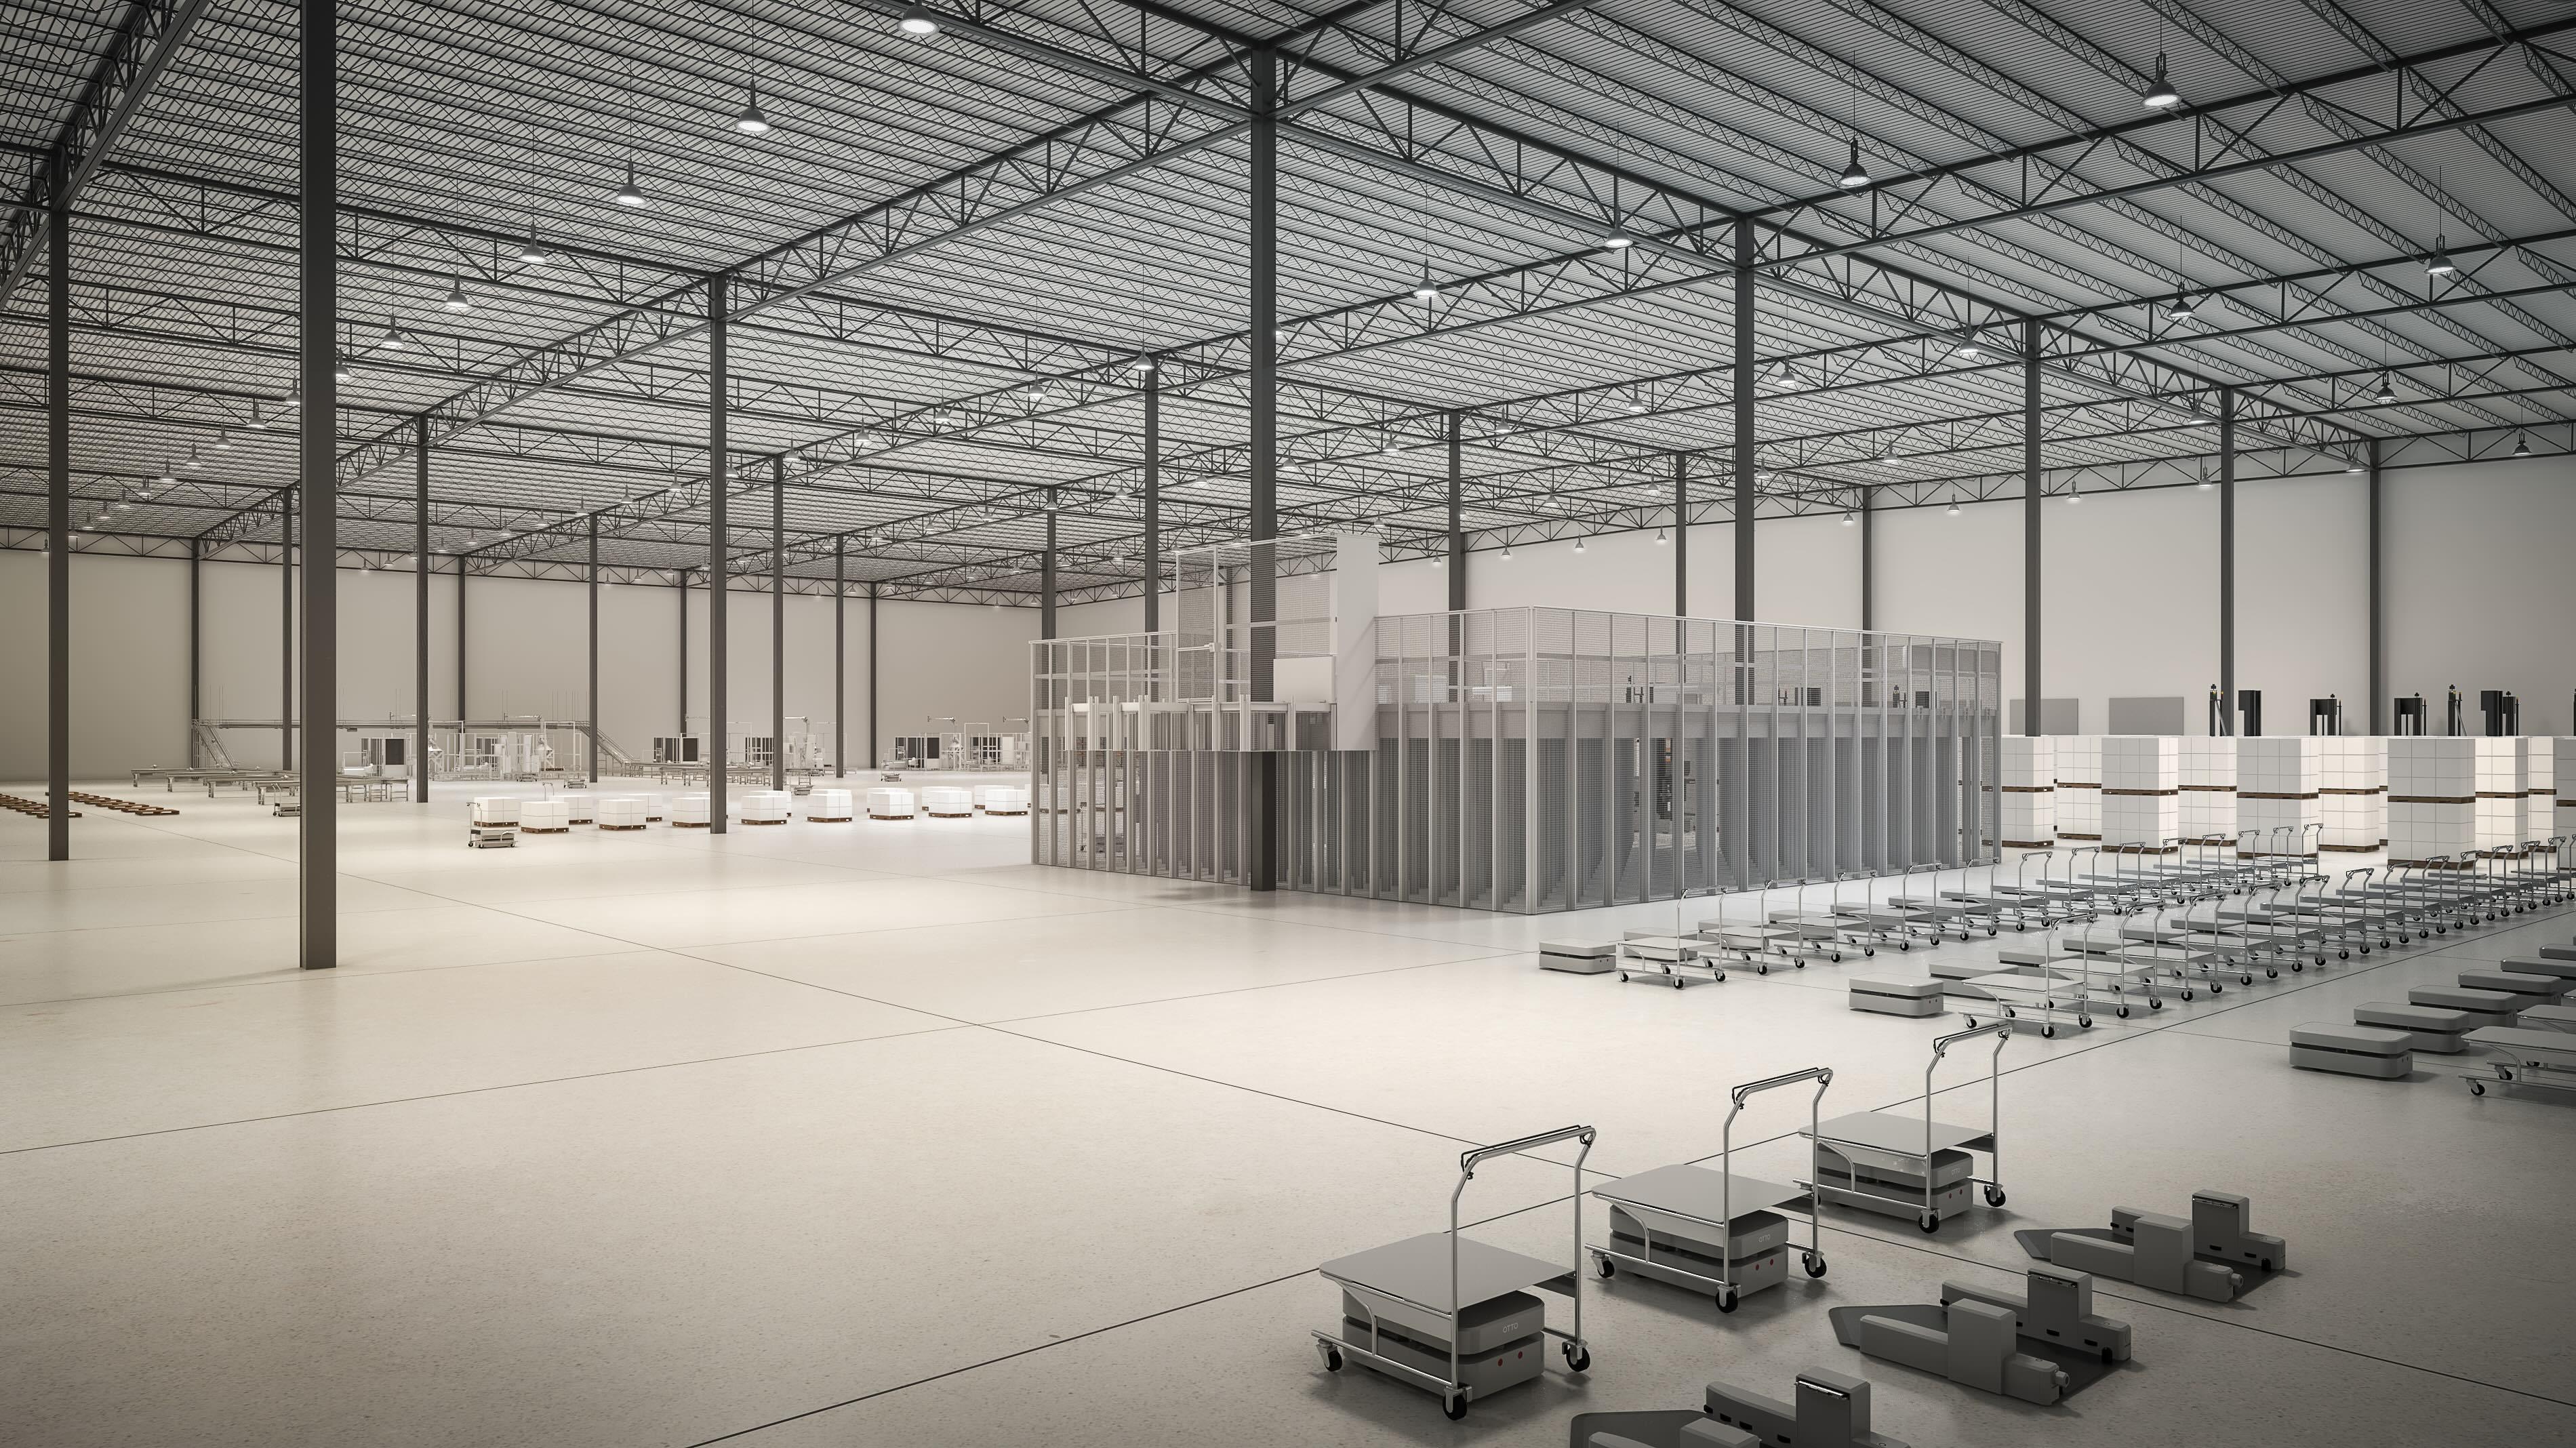
A leading food manufacturer needed to modernize a congested plant without stopping production. We integrated AMRs and automated forklifts across more than 30 packaging lines, improving material handling and packaging efficiency while operations kept running.